








A low casting price can disappear quickly when a gearbox housing distorts during machining, a coupling hub reveals shrinkage near the bore, or a bearing support develops porosity in a loaded wall. For power transmission component castings, the most useful records are the ones that connect the delivered heat and casting lot to the actual risks in service: material strength, internal soundness, geometry after stress relief, and repeatability from one production run to the next.
A certificate that merely states a material grade is rarely enough. The record should identify the heat, casting batch, part number, revision level, inspection method, acceptance basis, result, date, and release authority. Traceability is what turns a collection of reports into usable evidence. Without it, even a technically plausible test result may belong to a different melt, a different machining condition, or a different part configuration.
Start with the records that protect functional performance
Priority should follow the failure mode of the component rather than the length of the document package. A noncritical cover casting and a torque-carrying hub should not be reviewed with the same depth. Housings around rolling bearings need reliable bore geometry and stable wall sections. Gearcase castings need sound material around mounting faces, bearing seats, and load paths. Pulley bodies, sprocket centers, torque arms, and coupling components need evidence that the section carrying cyclic force is free from defects that machining or assembly could expose.
The most valuable documents generally fall into four connected groups: material certification, dimensional inspection, nondestructive examination, and process or repair records. Mechanical test data and heat-treatment records become especially important where the design relies on a specified strength, hardness range, ductility level, or controlled microstructure.
Material certificates: useful only when the heat is traceable
A material test report should state the cast alloy designation and the chemical analysis for the actual melt or heat associated with the parts. For gray iron, ductile iron, cast steel, and nonferrous alloys, the chemical report serves different purposes, but the same question applies: does the composition support the intended structure and properties?
For ductile iron, elemental chemistry alone does not establish nodularity, matrix condition, or tensile behavior. A report showing acceptable carbon, silicon, and alloy additions does not rule out poor nodule formation, carbide presence, uneven cooling effects, or section-sensitive properties. The mechanical-property report and, where specified, metallographic evidence carry the missing context.
For cast steel, chemistry needs to be read alongside heat treatment and mechanical tests. Carbon and alloy content influence hardenability and weldability, while section thickness affects how a heat-treatment cycle develops through the casting. A test coupon taken from a representative location is more meaningful than a detached result with no stated relationship to the delivered component.
Traceability details deserve close attention. Heat numbers should match the casting identification system used on the part or lot documents. If several heats are combined in one delivery, each part group should remain separable. A generic certificate copied across multiple batches creates uncertainty precisely when a field issue requires containment.
Mechanical test results need context, not just passing values
Tensile strength, yield strength, elongation, impact performance, and hardness records should be reviewed against the drawing or purchase specification. Yet a passing number can still be misleading when the test bar does not represent the section that governs service behavior. Thick hubs and thin ribs cool differently; the resulting matrix, grain structure, and residual stress state can differ within the same casting.
Hardness records are particularly easy to overread. A uniform hardness range may support machinability and wear expectations, but hardness does not prove freedom from cracks, inclusions, or internal voids. Conversely, a small hardness variation is not automatically a rejection issue if it falls outside a cosmetic expectation but remains within the functional requirement and reflects known section changes. The useful question is whether the result aligns with material grade, heat treatment, machining behavior, and the loaded area of the part.
Dimensional records should reflect the finished functional condition
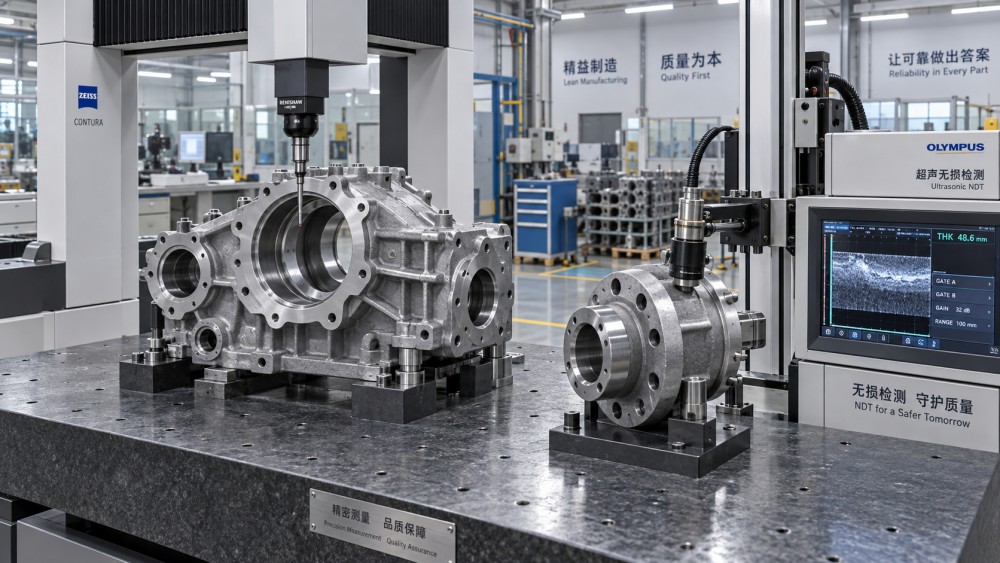
Dimensional inspection reports matter most when they cover the datums and features that locate, transmit, support, or seal. A broad list of external measurements offers little protection if the report omits the bearing bores, center distances, mounting planes, pilot diameters, shaft bores, keyway relationships, and runout controls that determine assembly behavior.
For a transmission housing, bore size alone is insufficient. The relationship between bores may control gear mesh, shaft alignment, bearing preload, and seal life. The inspection record should therefore identify datum references and report relevant positional or center-distance results, rather than presenting isolated diameters without orientation. For a coupling hub, the bore, keyway, concentricity, face runout, and axial location of the hub features often matter together. Measuring each feature independently can miss the stack-up that causes imbalance or misalignment.
Ask whether the report was generated before or after stress relief, rough machining, finish machining, coating, and any straightening operation. A casting may meet dimensions in the as-cast state yet move after machining releases residual stress. Likewise, paint can conceal a sharp edge, localized repair boundary, or deviation on a machined interface. The inspection stage must match the supplied condition.
Coordinate-measuring-machine reports can provide strong evidence when the programmed features, datum scheme, and actual measured points are clear. A simple pass/fail output is weaker than an inspection result that shows nominal dimension, tolerance, measured result, and equipment status. The latter makes it possible to judge whether a part is comfortably within tolerance or clustered near one limit.
Choose nondestructive examination by defect location and consequence
There is no single inspection method that proves a casting is sound everywhere. Visual examination, magnetic particle testing, liquid penetrant testing, ultrasonic testing, and radiography detect different defect types and work best in different conditions. A report is valuable when its method fits the part geometry and anticipated failure mode.
For heavily loaded regions, specify the inspection zone before production begins. “No internal defects” is too vague to administer. A drawing note or quality plan can identify critical areas such as the transition from hub to flange, a bearing-seat support wall, bolt circles near torque reactions, or thick junctions prone to shrinkage. The examination report should then show which zones were inspected and which acceptance criteria were applied.
Radiography is often associated with high assurance, but a radiograph is only as useful as the views selected and the section thickness it can resolve. A report covering one thick boss does not automatically validate an unexamined junction elsewhere. Ultrasonic examination can be effective for accessible material volumes, although curved geometry, coarse structure, and complex shapes may limit interpretation. Inspection records should disclose limitations rather than present a broad statement of conformance.
Repair history changes the meaning of otherwise acceptable results
Weld repair, impregnation, metal stitching, blending, and rework are not equivalent. Their acceptability depends on location, material, load path, machining allowance, and the agreed technical requirement. A repaired casting may be suitable for a low-stress external area yet unsuitable where fatigue loading crosses the repair zone or where pressure tightness is essential.
A repair record should identify the part, defect location, repair type, extent, authorization, procedure, post-repair inspection, and any heat-treatment or stress-relief action. “Repaired and accepted” gives no basis for judging whether a local indication was removed, whether new cracks were introduced, or whether a critical machined surface was affected.
Impregnation needs equal clarity. It can address distributed porosity in castings intended to retain lubricant or fluid, but it should not be treated as evidence that the underlying casting is structurally sound. Where an oil-filled gear housing requires leak resistance, pressure or leak-test records after machining and any impregnation provide more relevant evidence than a general statement about sealing treatment.
Process records expose repeatability before a recurring defect reaches assembly
First-article inspection is useful for confirming an initial setup, but it does not demonstrate continued control. For recurring parts, review lot-level evidence that links process stability to the characteristics that matter. This may include melt treatment records, pouring identification, heat-treatment charts, machining inspection summaries, and documented disposition of nonconforming parts.
The required depth should rise when the casting has thin-to-thick transitions, narrow tolerance relationships, safety-related loading, difficult-to-machine alloys, or a history of shrinkage and distortion. It can be lighter for a simple, lightly loaded casting with generous machining stock, provided the functional requirements are still verified on the finished part.
Heat-treatment charts deserve a practical review. They should show the cycle used, traceability to the lot, and any recorded deviations or interruptions. A chart with temperatures but no link to parts is incomplete. A chart linked to parts but lacking proof of instrument control leaves a separate gap. Neither record replaces mechanical testing where the specification calls for it; the documents answer different questions.
Read the document pack as a connected chain
The strongest release package allows a single delivered casting to be traced from identification mark to melt record, material results, heat treatment, nondestructive examination, dimensional inspection, repair disposition, and final release. Gaps often appear at handoffs: a casting is inspected before machining but shipped after machining; a repair is logged in production but omitted from final documentation; a dimensional report names the part but not the drawing revision.
Before accepting a lot, confirm that every report references the correct revision and supplied condition, that the sample quantity is stated, and that any exception has a documented disposition. A certificate showing conformity without the underlying measured characteristic is adequate only when the requirement and release process explicitly permit it. For features that determine torque transmission, bearing alignment, sealing, or fatigue life, recorded actual results carry much more weight.
Inspection records do not remove the need for incoming verification, especially for critical interfaces or new sources. They do establish where to focus that verification. When the documentation is traceable, method-appropriate, and tied to the finished functional features, cost comparisons become more credible because the quoted parts are being evaluated at a similar level of technical assurance.
Related News
- Buying Power Transmission Component Castings: Which Inspection Records Matter Most?Oct 12, 2026Power transmission component castings demand traceable inspection records. Learn which material, dimensional, NDT, and repair documents protect quality and reliability.
- Power Transmission Component Casting Defects That Shorten Gearbox Service LifeOct 11, 2026Power transmission component casting defects can trigger gearbox leaks, vibration, and bearing failure. Discover inspection priorities and repair-or-replace guidance.
- What to verify before choosing a chain drive systems supplierOct 01, 2026Chain drive systems supplier selection made easier: verify load analysis, standards, traceability, lubrication, quality control, and delivery reliability before buying.
- When does a low backlash transmission improve positioning accuracy?Sep 27, 2026A low backlash transmission improves positioning accuracy by reducing reversal error, enhancing settling, and supporting reliable precision motion.
Related News
- 00
0000-00
How to qualify a semiconductor equipment parts supplier for traceability - 00
0000-00
Which fluid power components for pneumatics suit high-cycle automation? - 00
0000-00
When do tighter tolerances justify precision manufacturing solutions for aluminum parts? - 00
0000-00
Buying Power Transmission Component Castings: Which Inspection Records Matter Most? - 00
0000-00
Power Transmission Component Casting Defects That Shorten Gearbox Service Life
Power Trans Designer
Strategic Intelligence Center