







Design Compliance with International Standards: What to Verify Before Tooling
Tooling is a commitment. Once a forging die, injection mold, stamping tool, machining fixture, or assembly gauge has been released, even a small misunderstanding in the design package can become expensive to correct. The issue is rarely limited to one incorrect dimension. A missing datum, an unclear material callout, or an unverified regional requirement can affect manufacturability, inspection strategy, supplier approval, field performance, and traceability.
For technical evaluators, design compliance with international standards is therefore not a final drawing-review activity. It is a pre-tooling discipline: confirming that engineering intent has been expressed in a way that can be manufactured, inspected, documented, and accepted across the intended supply chain. This is particularly important for precision components used in power transmission, fluid control, automated equipment, and other assemblies where fit, fatigue life, sealing, friction, or pressure containment depend on details that may appear minor on a drawing.
The practical objective is not to apply every available standard. It is to establish which standards govern the part, which requirements are contractual, which are functional, and where ambiguity must be resolved before metal is cut or tooling steel is purchased.
Start with the governing requirement hierarchy
A drawing may reference ISO, ASME, ASTM, EN, DIN, JIS, customer specifications, internal standards, and regulatory declarations at the same time. These references do not automatically have equal weight. Before tooling, the team should identify the hierarchy of documents and the applicable revision of each one. A purchase order, approved drawing, quality agreement, customer-specific requirement, and referenced standard can each define a different part of the acceptance criteria.
This matters when references appear compatible but are interpreted differently. Geometrical dimensioning and tolerancing practices under ISO GPS and ASME Y14.5 share many principles, but they should not be treated as interchangeable by assumption. Default rules, modifier usage, datum interpretation, and drawing conventions need to be read within the stated system. If the drawing mixes conventions, the issue should be closed through a documented clarification rather than left to the toolmaker or inspector.
A useful pre-tooling review asks a direct question: what exactly will determine acceptance at incoming inspection or final customer audit? If the answer is “the drawing, broadly speaking,” the package is not ready. Acceptance must be traceable to defined dimensions, tolerances, material conditions, test methods, sampling rules where applicable, and approved deviations.
Check whether the drawing communicates function, not only geometry
Nominal dimensions alone do not describe a functional part. A shaft seat for a bearing, a bore for a valve spool, a chain pin interface, or a hydraulic block sealing face performs according to relationships between features. Concentricity, runout, perpendicularity, profile, position, surface texture, edge condition, and datum structure can all influence the result.
The most revealing review is often an assembly-based one. Ask which surfaces locate the component in service, which faces transfer load, which features seal, and which dimensions control clearance or interference. Then compare those functional relationships with the datums and tolerances on the drawing. If a datum feature cannot be held consistently during manufacturing or inspection, it may be theoretically correct but commercially fragile.
General tolerances deserve the same scrutiny. A reference to a standard such as ISO 2768 may simplify a drawing, but it does not replace explicit tolerancing for critical features. General tolerances are appropriate only when the function can accept them. Applying them to a precision fit, a sealing land, a gear-related interface, or a controlled flow passage without additional definition invites variation that the tooling cannot intelligently prevent.
Surface requirements also need to be functional. A roughness value without the measurement direction, cutoff conditions, lay requirement, or relevant surface boundary may leave too much room for interpretation. For sliding, sealing, fatigue-sensitive, or coated surfaces, technical evaluators should verify whether the specified texture parameter actually reflects the intended operating condition. Surface indication conventions may refer to standards such as ISO 1302, but the drawing still has to identify where the requirement applies and whether the requirement is achievable after all planned processes.
Material compliance is more than selecting an alloy name
Material designation is frequently one of the weakest links in a tooling release. A familiar grade name may vary by standard system, product form, delivery condition, or equivalent designation. “Stainless steel,” “alloy steel,” or “engineering plastic” is never enough for a component with demanding mechanical, corrosion, wear, or thermal requirements.
The review should establish the governing material specification; required chemical composition or mechanical-property limits; product form; heat treatment or temper condition; and certification expectations. It should also identify whether the part will be cast, forged, rolled, bar-machined, sintered, molded, or additively produced, because the same nominal alloy can behave differently across process routes.
For hardened and wear-critical components, hardness alone may not be sufficient evidence of compliance. Case depth, core condition, microstructure, distortion risk, grinding allowance, and decarburization limits may need separate definition depending on the application. In fluid-control parts, compatibility between the base material, plating or coating, process media, cleaning method, and expected fluid is equally relevant. A coating specified to improve corrosion resistance can create dimensional change, adhesion concerns, hydrogen-related risk in certain process chains, or unwanted effects on a sealing interface.
Environmental declarations should be reviewed early rather than added after tooling approval. Requirements related to restricted substances, material traceability, recycled-content claims, or market-specific chemical obligations are not universal and should be confirmed against the destination market and customer contract. The correct question is not whether a part is “globally compliant,” but which documented obligations apply to this component in this application.
Tooling feasibility must include process variation
A compliant drawing can still be a poor tooling candidate if it ignores how the material and process move. Tooling review should consider shrinkage, springback, machining deflection, mold-flow behavior, die wear, grain flow, thermal distortion, and the sequence of secondary operations. These factors do not excuse nonconformance; they determine whether the selected process can reliably achieve conformance.
Consider a part that requires a tight positional relationship between a formed feature and a later-machined bore. If the locating strategy is based on an unstable formed edge, the component may meet individual dimensions while missing the functional relationship. The tooling concept should show how datums are transferred from one operation to the next and how any expected movement is controlled or compensated.
Tolerances should also be classified by purpose. Some protect fit or safety. Others reflect legacy drawing practice, aesthetic preference, or an earlier manufacturing method. Tightening every dimension is not a sign of robust engineering. It can increase inspection burden, reject acceptable variation, and lead suppliers to rely on sorting instead of process control. Before tooling, each tight tolerance should have a defensible functional reason and an agreed measurement method.
Measurement capability is part of the design decision
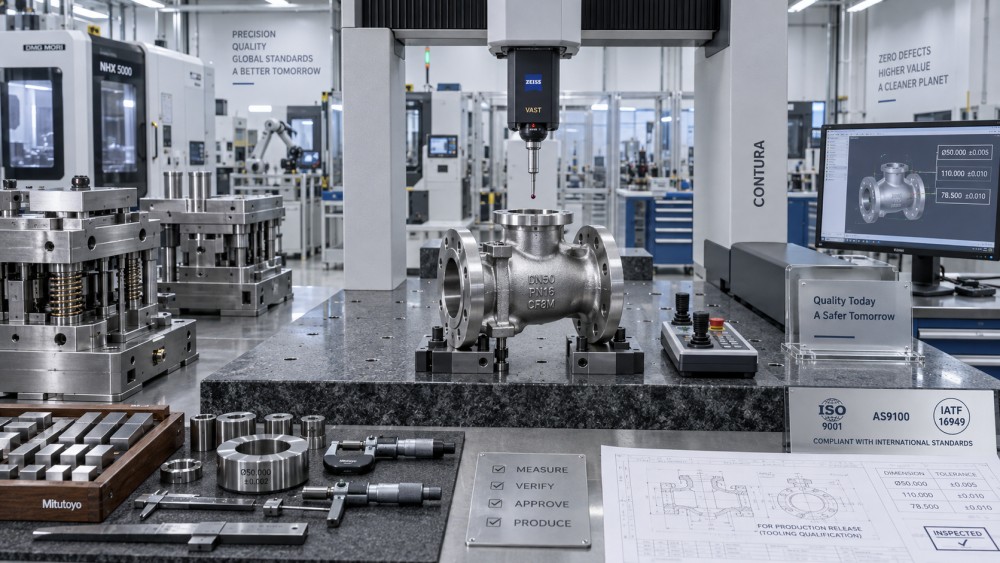
If a feature cannot be measured repeatably, compliance cannot be demonstrated reliably. This point is especially important for freeform profiles, small radii, internal passages, thin-wall parts, deep bores, complex castings, and surfaces affected by flexible material behavior. The inspection plan should be reviewed before tooling release, not written after the first samples arrive.
Technical evaluators should confirm the inspection datum scheme, gauge access, equipment suitability, calibration requirements, and the relationship between the drawing tolerance and the anticipated measurement uncertainty. Coordinate measuring machines, optical systems, air gauges, functional gauges, pressure tests, and surface instruments can all be appropriate, but they do not produce equivalent evidence. A functional gauge may efficiently verify assembly fit, while a variable measurement may be necessary to understand process drift.
Where special characteristics are identified, the control method should be explicit. The drawing symbol alone is not a control plan. The supplier and customer still need agreement on what is measured, at which stage, by which method, and what records are retained. In sectors that use structured approval processes, such as PPAP or customer-specific first-article packages, required submission content should be known before the production tool is built.
Do not separate compliance from the supply chain
International sourcing introduces a practical layer beyond standards interpretation. Material availability, local test capabilities, subcontracted heat treatment, plating capacity, export controls, transport conditions, and documentation practices can affect whether the specified design is realistically supportable. A technically valid material or treatment may have limited availability in a particular manufacturing region, longer qualification lead times, or a supply route that complicates traceability.
That does not mean specifications should be weakened for convenience. It means alternatives must be evaluated transparently. Any proposed substitution should be assessed against functional properties, manufacturing response, applicable standards, and customer approval requirements. “Equivalent” is not a sufficient engineering conclusion without defining equivalent in relation to the actual service conditions.
This is one area where intelligence across materials, motion systems, and fluid-control technologies becomes useful. GPCM examines the underlying decisions that connect tolerances, material science, process capability, and market supply conditions. Its Strategic Intelligence Center follows developments in areas such as high-performance composite bearings, maintenance-free chains, and high-pressure integrated hydraulic valve blocks—component categories where design choices and production constraints are tightly linked. For evaluators, the value lies in using such cross-disciplinary context to identify questions earlier, before a supplier’s quotation becomes a tooling commitment.
A practical release gate before tooling authorization
A disciplined release gate does not need to be bureaucratic, but it should produce clear answers. The design package is generally ready for tooling only when the applicable standard system and document revisions are identified; functional datums and critical characteristics are unambiguous; material and finish requirements are tied to verifiable specifications; the intended manufacturing route is feasible; and the inspection approach can confirm the required characteristics.
Open questions should be recorded as engineering decisions, not buried in email threads or supplier assumptions. This includes permissible process changes, cosmetic limits, deburring expectations, marking requirements, packaging constraints, sample approval criteria, and the authority permitted to accept deviations. A controlled clarification may seem slow before tooling, but it is usually much faster than correcting hardened tooling or disputing whether an inspection result reflects the part or the interpretation.
The strongest pre-tooling reviews treat compliance as a translation exercise. They translate product intent into material behavior, process capability, measurable criteria, and supply-chain evidence. When those links are visible, tooling decisions become more predictable—and the finished component is far less likely to reveal a standards problem after production has already begun.
Related News
- Design Compliance with International Standards: What to Verify Before ToolingOct 17, 2026Design compliance with international standards: verify drawings, materials, tolerances, tooling feasibility, and inspection plans before production begins.
- How Do Industrial Regulations Affect Component Material Selection?Oct 15, 2026Do industrial regulations affect component material selection? Explore how compliance, safety, traceability, and global standards shape smarter material decisions.
- How to verify regulatory compliance for semiconductors before launchSep 26, 2026Regulatory compliance for semiconductors: learn how to verify materials, exemptions, traceability, trade controls, and market readiness before launch.
- What should count most in supplier compliance evaluation criteria?Sep 19, 2026Supplier compliance evaluation criteria: prioritize product conformity, traceability, change control, and delivery readiness to reduce risk and build resilient supply chains.
Related News
- 00
0000-00
When do precision ground gears reduce noise in high-speed gearboxes? - 00
0000-00
How pressure ratings affect the price of flow control components - 00
0000-00
How to choose gear materials for high-load industrial gearboxes - 00
0000-00
How to choose engineering plastics for gears without lubrication - 00
0000-00
How to vet North American fluid dynamics engineering firms for CFD
Tribology Specialist
Strategic Intelligence Center