



OEM export quality should be evaluated as a control system with evidence, not as a statement on a quotation or a sample approval. A component can look correct at dispatch while still carrying expensive exposure: mixed material lots, an unverified process change, measurement methods that miss functional variation, or packaging that permits corrosion during transit. The practical question is whether the supplier can repeatedly release conforming parts after the order moves from first article to routine production.
Cost decisions belong inside that question. A lower unit price loses its advantage when incoming inspection expands, assembly stoppages occur, replacement shipments are needed, or a field failure cannot be traced to a production lot. Conversely, a higher quoted price does not prove stronger control. The useful comparison is the cost of obtaining a verifiable, stable part at the required delivery condition.
Start with the controls behind the sample
Approved samples are valuable, but they show only one point in time. They may have been produced on a different machine, with selected material, extra inspection, or manual adjustment that will not be present during normal runs. An audit should establish whether the same routing, tooling, gauges, operators' instructions, and release criteria will govern serial output.
Ask to follow one representative part through the actual sequence: receipt of raw material, cutting or forming, machining, heat treatment or coating where applicable, washing, final inspection, preservation, packing, and shipment release. The route does not need to be complex to be controlled. What matters is that each quality-sensitive handoff is identifiable and that records connect it to the finished lot.
A supplier that relies on experienced operators without current work instructions may make acceptable parts until a shift changes, a tool wears, or a rush order is introduced. In contrast, a dense document set has limited value when it is disconnected from the shop floor. Revision status should match between the purchase specification, drawings, process sheets, inspection plan, and labels attached to work in progress.
Separate product characteristics by consequence
Not every dimension merits the same control. An overall length with generous clearance can be inspected by sampling without carrying the same risk as a bearing-seat diameter, sealing land, gear tooth profile, mating thread, flatness requirement, or hydraulic passage. A useful audit asks how the supplier identifies characteristics that affect fit, load path, leakage, torque transmission, safety, or downstream automation.
Critical features need more than a final pass/fail entry. Review where they are measured, how frequently, which gauge is used, what action occurs when a trend approaches a limit, and whether affected production can be isolated. A final inspection record that lists compliant values does not reveal whether variation was controlled throughout the run or merely sorted at the end.
Tolerance interpretation also requires functional context. A shaft diameter can meet its drawing limits yet create an unacceptable assembly if surface finish, roundness, taper, coating thickness, or burr condition are ignored. A machined valve body can meet external dimensions while an imperfectly cleaned internal passage later damages a seal or restricts flow. The audit should compare the inspection plan with the part's actual interface and service duty, rather than treating each drawing callout as independent.
Traceability must work backwards and forwards
Material traceability is often described too broadly. The relevant standard is not simply whether paperwork exists, but whether a finished shipment can be linked back to its actual incoming material and whether a suspect material batch can be linked forward to all affected finished lots. This distinction becomes urgent when alloy grade, heat treatment response, corrosion resistance, or pressure capability depends on the exact raw material source.
Traceability depth should match the failure mechanism. A simple non-load-bearing stamped cover may need lot identification and receiving verification. A fatigue-loaded pin, precision bearing ring, welded pressure component, or hardened transmission part demands a stronger chain between material certificate, heat or melt reference, production batch, process records, and shipment label. If material is split, blended, relabeled, or moved into unmarked containers, the chain can break even while all documents appear complete.
During the audit, select a finished carton or pallet at random and ask for its production and material history. Then begin with an incoming material record and request the finished lots into which that material was consumed. Delays, reliance on memory, or a need to reconstruct identifiers manually reveal a control weakness. The same exercise should cover outsourced operations such as plating, heat treatment, grinding, molding, or non-destructive testing.
Material and special processes deserve direct scrutiny
Material substitutions are a recurring source of hidden export quality risk. Similar commercial names do not ensure equivalent composition, cleanliness, mechanical properties, or heat-treatment response. The risk increases when a material is selected for wear, fatigue, temperature, corrosion, electrical conductivity, or compatibility with oils and process fluids. A substitution cannot be accepted merely because it is available, lower cost, or close in nominal grade.
Review receiving controls for identity, condition, quantity, and certificate reconciliation. For bar stock, forgings, castings, polymers, seals, and coated sheet, verify how the supplier prevents acceptance of unapproved alternatives. Material held for inspection should be visibly segregated from released stock. Scrapped or returned material requires equal attention; without clear disposition, it can re-enter production as usable inventory.
Special processes can alter a part beyond what final dimensional inspection will expose. Heat treatment affects hardness distribution, distortion, residual stress, and microstructure. Coating can change thread fit, surface friction, corrosion behavior, and contact dimensions. Welding may introduce distortion, incomplete fusion, or variation linked to joint preparation and consumables. Washing and preservation influence particulate contamination and corrosion during sea or air transit. The audit should identify the process parameters that matter and determine whether they are recorded against the lot.
Outsourcing does not transfer responsibility away from the export supplier. A supplier may use capable external processors, but it should have defined approval criteria, purchase requirements, incoming acceptance methods, and a way to quarantine nonconforming returns. Repeated reliance on certificates without verification can be acceptable only where the risk and established processor control justify it; it is not a universal substitute for oversight.
Measurement systems can create false confidence
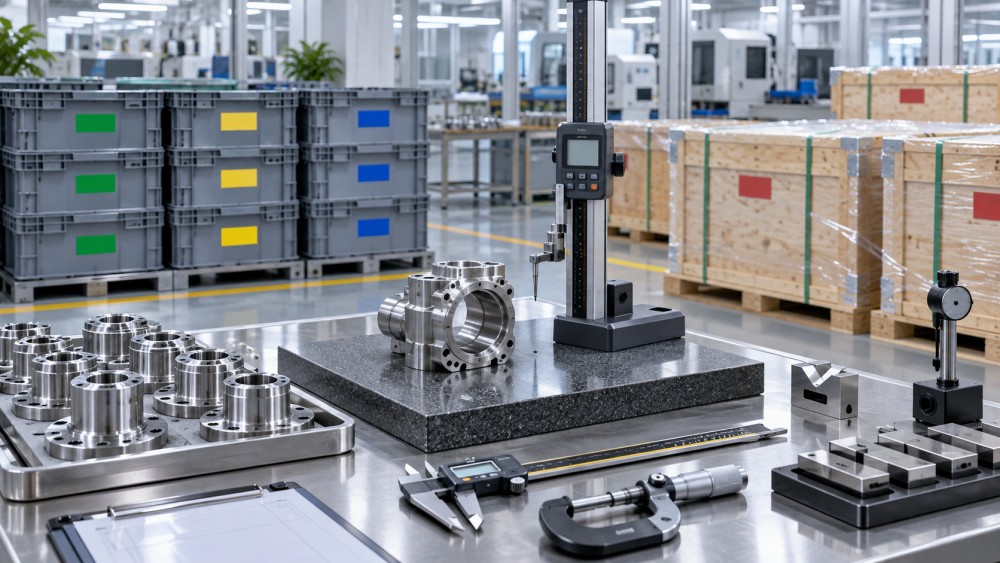
Inspection data is only as sound as the method that produces it. A digital caliper may be adequate for a broad external dimension but unsuitable for a close bore, datum-sensitive geometry, rough surface, or soft component that deforms under contact. Coordinate measurement may provide detailed output while still producing misleading results if fixturing, datum alignment, probing strategy, temperature, or program revision is poorly controlled.
Examine the relationship between tolerance width and measurement capability. When the gauge resolution is too coarse, or repeat readings vary enough to consume a meaningful share of the tolerance, the recorded result cannot support confident release. Ask for evidence that gauges are identified, maintained, and checked at suitable intervals. Calibration labels alone do not prove that the chosen instrument measures the characteristic correctly.
There is also a difference between inspection of a part and verification of an assembly condition. A thread gauge can confirm basic acceptability, yet not detect damage caused by plating buildup or handling. A go/no-go gauge may efficiently protect a functional interface but gives little information about drift toward its rejection boundary. For high-consequence characteristics, variable data from the production run can show whether the process is centered and stable. The expected evidence should reflect the consequence of a failure rather than a preference for a particular reporting format.
Control change before it becomes a shipment issue
Many quality failures originate in changes that appear operationally minor: a new cutting tool supplier, alternate resin, revised plating source, fixture repair, machine relocation, altered curing cycle, or a change in subcontract processor. Some changes have no effect on the finished part; others alter capability or durability without being visible at receiving inspection. The important issue is whether there is a defined method to evaluate a change before production is released.
Review how changes are classified, approved, documented, and communicated. The process should distinguish routine replacement of equivalent consumables from changes to material source, process parameters, inspection method, tooling geometry, manufacturing location, or external processing. Where a characteristic is functional, approval may require a new first article, capability evidence, fit check, or performance test appropriate to the change. An informal assurance that "nothing changed" is weak when the factory has no controlled mechanism for recording changes.
Order documents should state the notification requirement in practical terms. Requiring notice for every internal action creates noise and encourages noncompliance. Limiting notification to changes that affect approved material, process route, plant location, tooling affecting form or fit, external processor, inspection method, or declared performance creates a more usable boundary.
Nonconformance handling reveals operating discipline
Every production environment encounters defects. The deciding issue is whether a nonconforming condition is contained quickly, assessed against all potentially affected stock, and prevented from recurring through a verified corrective action. A clean audit area with no visible rejection records is not automatically reassuring; it can mean that problems are not formally captured.
Request a recent closed nonconformance record, with commercially sensitive details removed if necessary. It should show the issue description, containment action, affected lot identification, disposition, root-cause reasoning, corrective action, responsible owner, and evidence that the action was effective. A response that ends with retraining or increased inspection may be appropriate for an isolated handling error, but it does not resolve recurring variation caused by worn equipment, ambiguous instructions, unsuitable fixturing, or a weak incoming control.
Containment must cover material already packed or shipped as well as work in process. If a defect is found after dispatch, the supplier needs a defined method to identify shipment references, communicate scope, provide replacement information, and preserve records. This is particularly relevant for export shipments with long transit periods, where delayed discovery can overlap with subsequent production lots.
Release condition includes packing and transport exposure
A conforming component can arrive unusable if its export packing does not protect its actual vulnerabilities. Machined ferrous parts may need preservation compatible with expected transit duration and destination humidity. Precision surfaces require separation that prevents metal-to-metal contact. Seals, polymers, and adhesives may need limits on heat, ultraviolet exposure, compression, or contamination. Heavy parts need restraint that prevents movement without placing point loads on finished surfaces.
Assess packaging as part of the control plan. Confirm that the part number, revision, quantity, lot reference, and handling status remain legible after packing. Mixed lots in one carton can be efficient, but only where label structure and internal separation allow traceability to survive receiving and line-side use. Packaging changes should receive the same review as other changes when they affect corrosion protection, cleanliness, damage risk, or identification.
Convert audit observations into a sourcing decision
Audit results are most useful when they distinguish between missing evidence, contained weaknesses, and systemic exposure. A missing scan of one calibration record is different from an inspection system that cannot link gauges to part characteristics. A process document awaiting revision is different from a factory that routinely runs parts to obsolete instructions. Findings should be recorded with the affected part family, failure consequence, available containment, evidence reviewed, and the action required before release.
Commercial comparison should then include the controls needed to close the gap. Additional incoming inspection, third-party verification, tighter packaging requirements, lot-level certificates, trial batches, or staged release can be reasonable cost items when risk is not yet proven low. These measures should not become permanent substitutes for a capable production system.
Strong OEM export quality is visible in ordinary records and routine behavior: material stays identified, critical characteristics are measured by suitable methods, process changes are controlled, defects are traceable, and shipment condition is treated as part of product conformity. When those controls can be demonstrated across a normal production lot, price comparisons rest on a more credible basis.
Related News
- OEM Export Quality: A Buyer’s Framework for Auditing Supplier ControlsOct 20, 2026OEM export quality starts with verifiable supplier controls. Explore a buyer’s framework for auditing traceability, measurement, process changes, packaging, and sourcing risk.
- How to build a product category guide for Latin American marketsOct 09, 2026Product category guide Latin America: learn how to build localized, application-led industrial product guides that improve buyer confidence, distributor sales, service clarity, and regional growth.
- How to assess delivery reliability when sourcing from EuropeOct 03, 2026Delivery reliability assessment Europe: learn how to verify supplier capacity, material availability, communication, and logistics before sourcing critical components.
- How the global trade environment is reshaping export market accessSep 30, 2026Global trade environment insights for exporters: learn how tariffs, origin rules, compliance, and supply-chain resilience reshape sustainable market access.
Related News
- 00
0000-00
Can distributors profit from low-volume private label components? - 00
0000-00
Can fluid power systems for robotics deliver precise motion control? - 00
0000-00
How to control design changes when working with an OEM supplier - 00
0000-00
When do precision ground gears reduce noise in high-speed gearboxes? - 00
0000-00
How pressure ratings affect the price of flow control components
Ms. Elena Rodriguez
Strategic Intelligence Center